Drill series extended with interchangeable drill head dedicated to cast iron

2 Mins
Published in Tooling
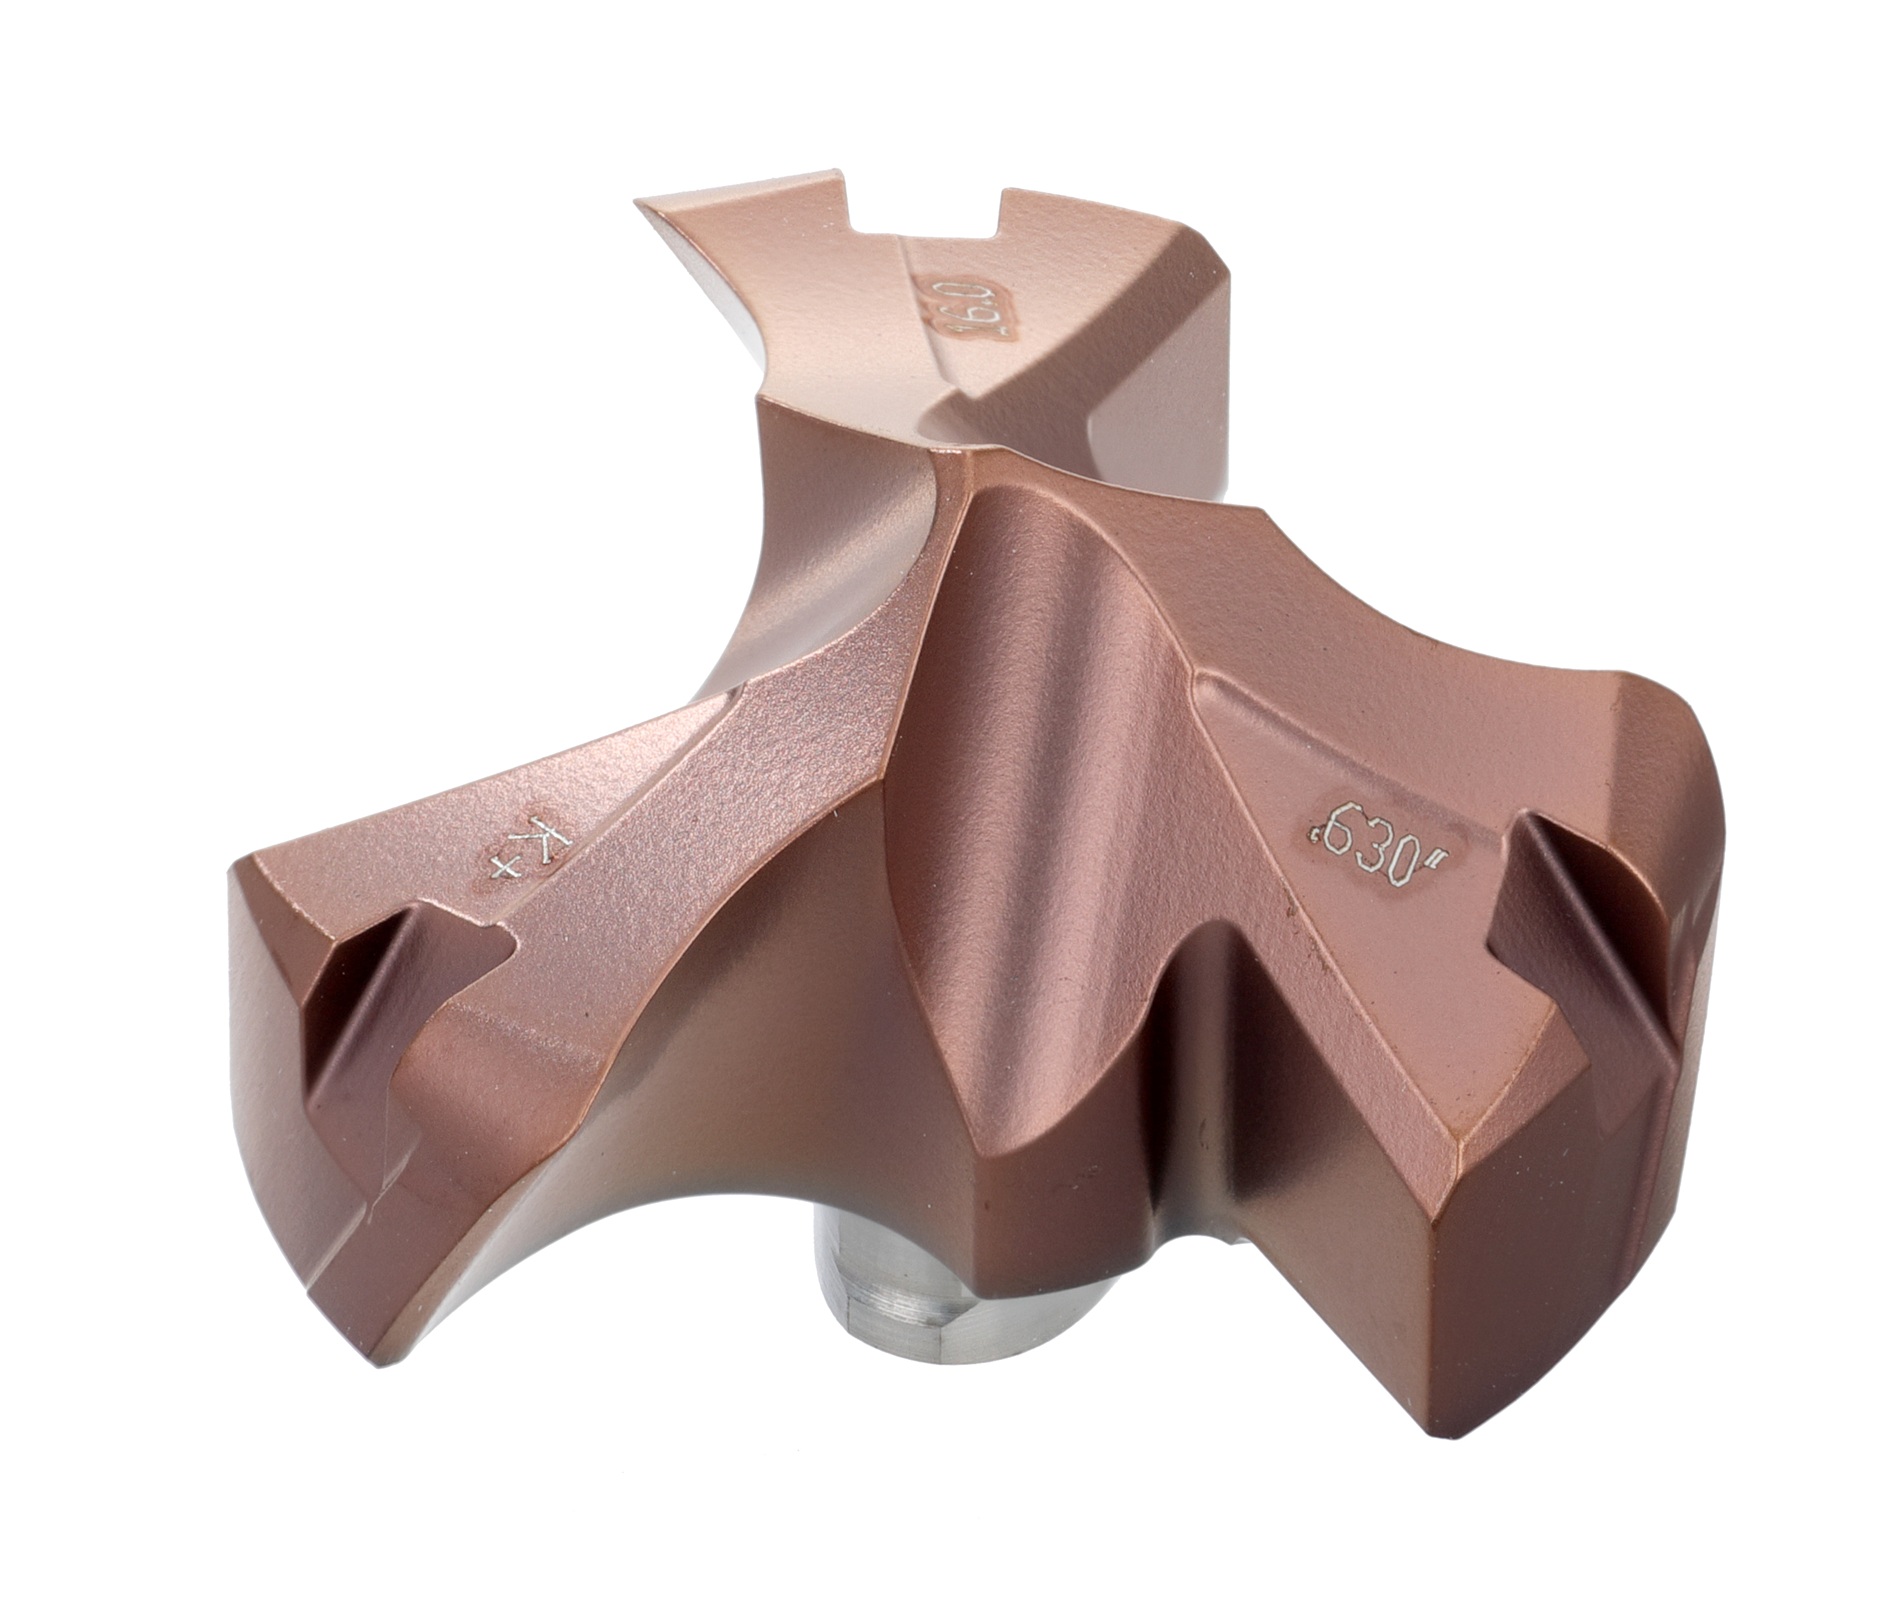
TaeguTec has extended its DRILL-SFEED indexable 3-flute drill system by introducing the 3ED-K+ head, a new interchangeable drill head engineered for cast-iron machining. The addition completes the DRILL-SFEED head family, alongside the existing 3ED-P+ general-purpose head and the 3ED-F flat-bottom variant, providing manufacturers with a dedicated, optimised solution for grey, nodular and malleable cast-iron applications.
With the relentless rise in carbide costs, the indexable 3-flute DRILL-SFEED is for aids the productive, cost-effective drilling of cast iron. The 3ED-K+ head features optimised cutting-edge geometry tailored to the specific characteristics of cast iron. This material demands precise edge preparation and advanced coating technology to achieve consistent hole quality and extend tool life.
The K+ design delivers the same reliable self-centring capability as the P+ head, ensuring positional accuracy on entry without the need for a pilot hole. A quick-change head system allows worn heads to be replaced in seconds without removing the holder from the machine, minimising downtime and keeping spindles cutting.
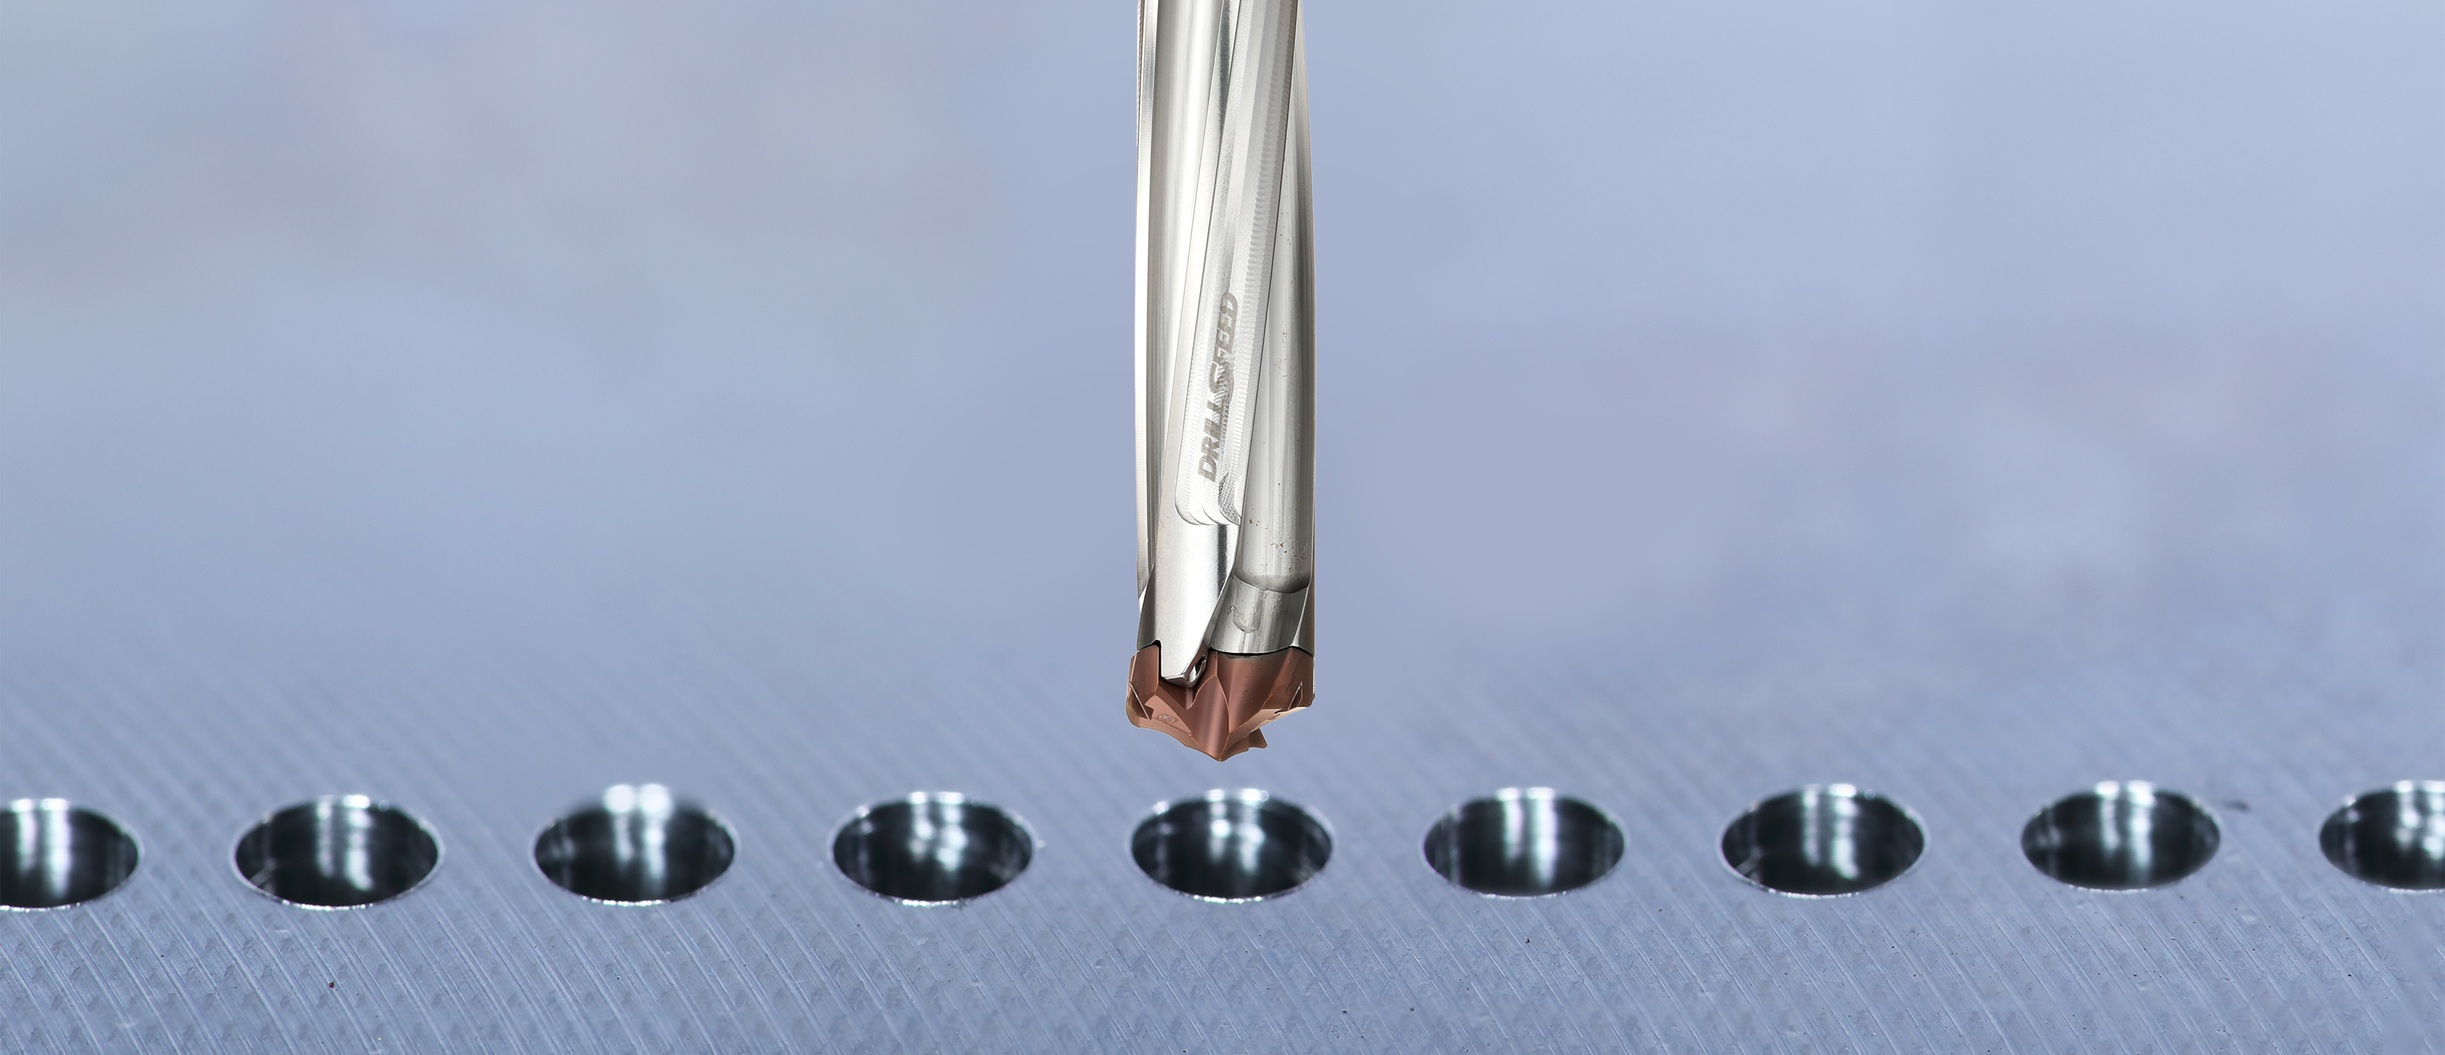
The new K+ head delivers impressive results compared with the general-purpose P+ alternative when machining cast iron. On nodular cast iron, the 3ED-K+ achieved a tool life of 100.8 minutes, compared with 65.8 minutes for the P+ head, a 53% improvement under identical cutting conditions of 110 m/min, 0.7 mm/rev feed and 50 mm depth of cut at 16 mm diameter. Under test conditions using TaeguTec’s TT5130 grade, K+ head geometry has proven to be a clear differentiator in driving these performance gains.
The 3ED-K+ heads are available from stock in 0.5 mm diameter increments from 12.0 to 25.5 mm diameter, with inch-size variants also included in the range. All heads are compatible with standard DRILL-SFEED holders in 3xD, 5xD and 8xD configurations, providing versatility across a wide range of hole depths without any change to existing tooling investment. Recommended cutting speeds range from 80 to 180 m/min, depending on the cast iron grade and condition, with feed rates from 0.3 to 0.7 mm/rev, scaling with diameter.
Want to know more about this article?
Ask us below...